What Is Stripe Coating? Steel Details That Need Attention
Stripe coating usually means applying additional, localized coating to steel details that are difficult to cover evenly, such as edges, welds, and fasteners. It supports continuous protection at vulnerable locations while the full coat covers the broader surface.
A freshly painted structure can look uniform yet have weak coverage around a connection or sharp corner. However, the details requiring special treatment depend on the coating system, project specification, and applicable standard, so the first distinction is between localized protection and full-surface coverage.
How Stripe Coating Differs From a Full Coat
Localized coverage addresses difficult geometry
A stripe coat concentrates coating on selected details rather than the entire steel surface. The purpose is to improve coverage where shape, surface irregularities, or restricted access make an even film harder to achieve.
For example, the transition between a weld bead and surrounding plate needs different attention than an open, flat panel. Likewise, a bolt assembly presents several small faces and recesses within a compact area.
These locations need deliberate attention when the specification calls for it. However, the term doesn't establish a universal application method, coating product, or acceptance requirement.
The full coat protects the broader surface
The full coat covers the designated surface as part of the specified coating system. Depending on the system, that broader work can involve primer, intermediate coating, or finish material.
Localized treatment doesn't replace full coverage. It also doesn't make up for missed preparation, incompatible materials, or inadequate coating elsewhere.
When comparing proposals, distinguish detail treatment from the overall coating scope. A promise to address edges and welds should accompany a clearly described system for the entire structure.
Why Steel Details Are Harder to Protect
Edges and corners can develop thin coverage
Sharp outside edges can retain less coating than nearby flat surfaces. As wet material flows and dries, coverage at an edge may become thinner than the surrounding film.
Inside corners create a different challenge. Restricted access can make complete coverage difficult, while excessive material may collect in the recess.
As a result, a surface that looks evenly colored may still have uneven protection. Edge condition, coating behavior, and access all affect the outcome. Where the specification requires edge preparation, additional coating alone doesn't replace that preparation.
Welds and fasteners create uneven surfaces
Weld beads, weld toes, bolt heads, nuts, and washers interrupt otherwise straightforward steel surfaces. Their changes in direction create places where coating can be missed or distributed unevenly.
Meanwhile, weld spatter and rough fabrication defects can interfere with coating continuity. Fastener assemblies also contain interfaces that an exterior coating cannot necessarily reach.
This matters because moisture and contaminants can collect around connections. The coating plan should address both accessible surfaces and any separate joint-treatment requirements, rather than assume exterior paint will protect concealed contact areas.
Which Steel Details Deserve Extra Attention?
The following details commonly warrant consideration during coating planning. Their presence alone doesn't establish a mandatory stripe-coating requirement.
| Steel detail | Why coverage needs attention |
|---|---|
| Plate edges and outside corners | Sharp geometry can leave thinner coverage than adjacent flat steel. |
| Inside corners and recesses | Restricted access can leave missed areas or uneven buildup. |
| Weld beads and weld toes | Irregular contours make continuous coverage harder to achieve. |
| Bolt heads, nuts, and washers | Multiple faces and tight transitions complicate coverage. |
| Brackets, stiffeners, and connection plates | Closely spaced components can obstruct access to the steel. |
| Seams and accessible connection boundaries | Interfaces can retain moisture and need a defined treatment detail. |
The important distinction is between identifying a vulnerable detail and deciding how to protect it. Preparation, localized coating, compatible joint treatment, or repair may address different parts of the problem.
On storage tanks, these locations belong within the broader exterior tank recoating scope. Fittings, supports, and connections need attention alongside the shell, but exterior coating work doesn't automatically include interior lining or structural repairs.
Pitted steel also needs assessment before coating. Additional material cannot restore metal that corrosion has already removed.
Surface Preparation Comes Before Detail Coating
Start with clean, sound steel
Extra coating won't bond reliably over oil, salts, loose rust, mill scale, or failed paint. The preparation scope should identify which contaminants and unsound materials require removal, along with the required cleanliness and surface profile.
For example, SSPC-SP 10/NACE No. 2 describes near-white blast cleaning of steel. That reference defines a preparation level; it doesn't automatically apply to every project.
Our guidance on coatings for wastewater service areas explains why preparation must match the substrate and exposure. The same principle applies to small steel details: their size doesn't make surface condition less important.
Address defects before covering them
Sharp edges, weld irregularities, loose corrosion, and deteriorated connections need defined treatment before coating begins. Depending on their condition, some details may require fabrication correction or qualified repair rather than additional paint.
Likewise, deep pitting, distortion, damaged supports, or suspected loss of metal thickness can require professional assessment. Coating work doesn't establish structural integrity.
Preparation also includes transitions into sound existing coating when the project retains it. Abrupt ridges, weak edges, and incompatible old finishes can undermine the new work.
A complete scope separates surface preparation from repairs so owners can see what each activity accomplishes.
Let the Coating System and Specification Set Requirements
There isn't one stripe-coating rule for every steel railing, tank, pipe, or structural frame. Exterior exposure, immersion, chemical contact, and washdown create different service conditions.
The written scope should connect those conditions to the selected products and applicable requirements. It should identify the details receiving localized treatment, how that treatment fits the coating sequence, and how the completed work will be assessed.
Coating compatibility matters throughout the system. A material suitable for broad exterior steel isn't automatically suitable for an immersed lining or a chemically exposed connection.
Application controls matter, too. Mixing ratios, required induction periods, pot life, recoat limitations, and environmental conditions come from the selected system's requirements. Missing a recoat window can create additional preparation work before coating continues.
Weather planning must cover the vulnerable curing period as well as application. Morning dew, rain, wind, and sun-heated steel can affect the available work window.
An acceptable reading on an open steel panel doesn't establish acceptable coverage around the nearby welds and fasteners.
For owners comparing bids, a lower price may omit detail work, access equipment, preparation, or inspection. Our industrial painting and coating services help facilities in Southwest Florida determine appropriate coatings and finishes. A useful proposal translates that selection into a defined scope, rather than a general promise to paint the steel.
Inspection Must Look Beyond a Uniform Finish
Assess coverage and film thickness
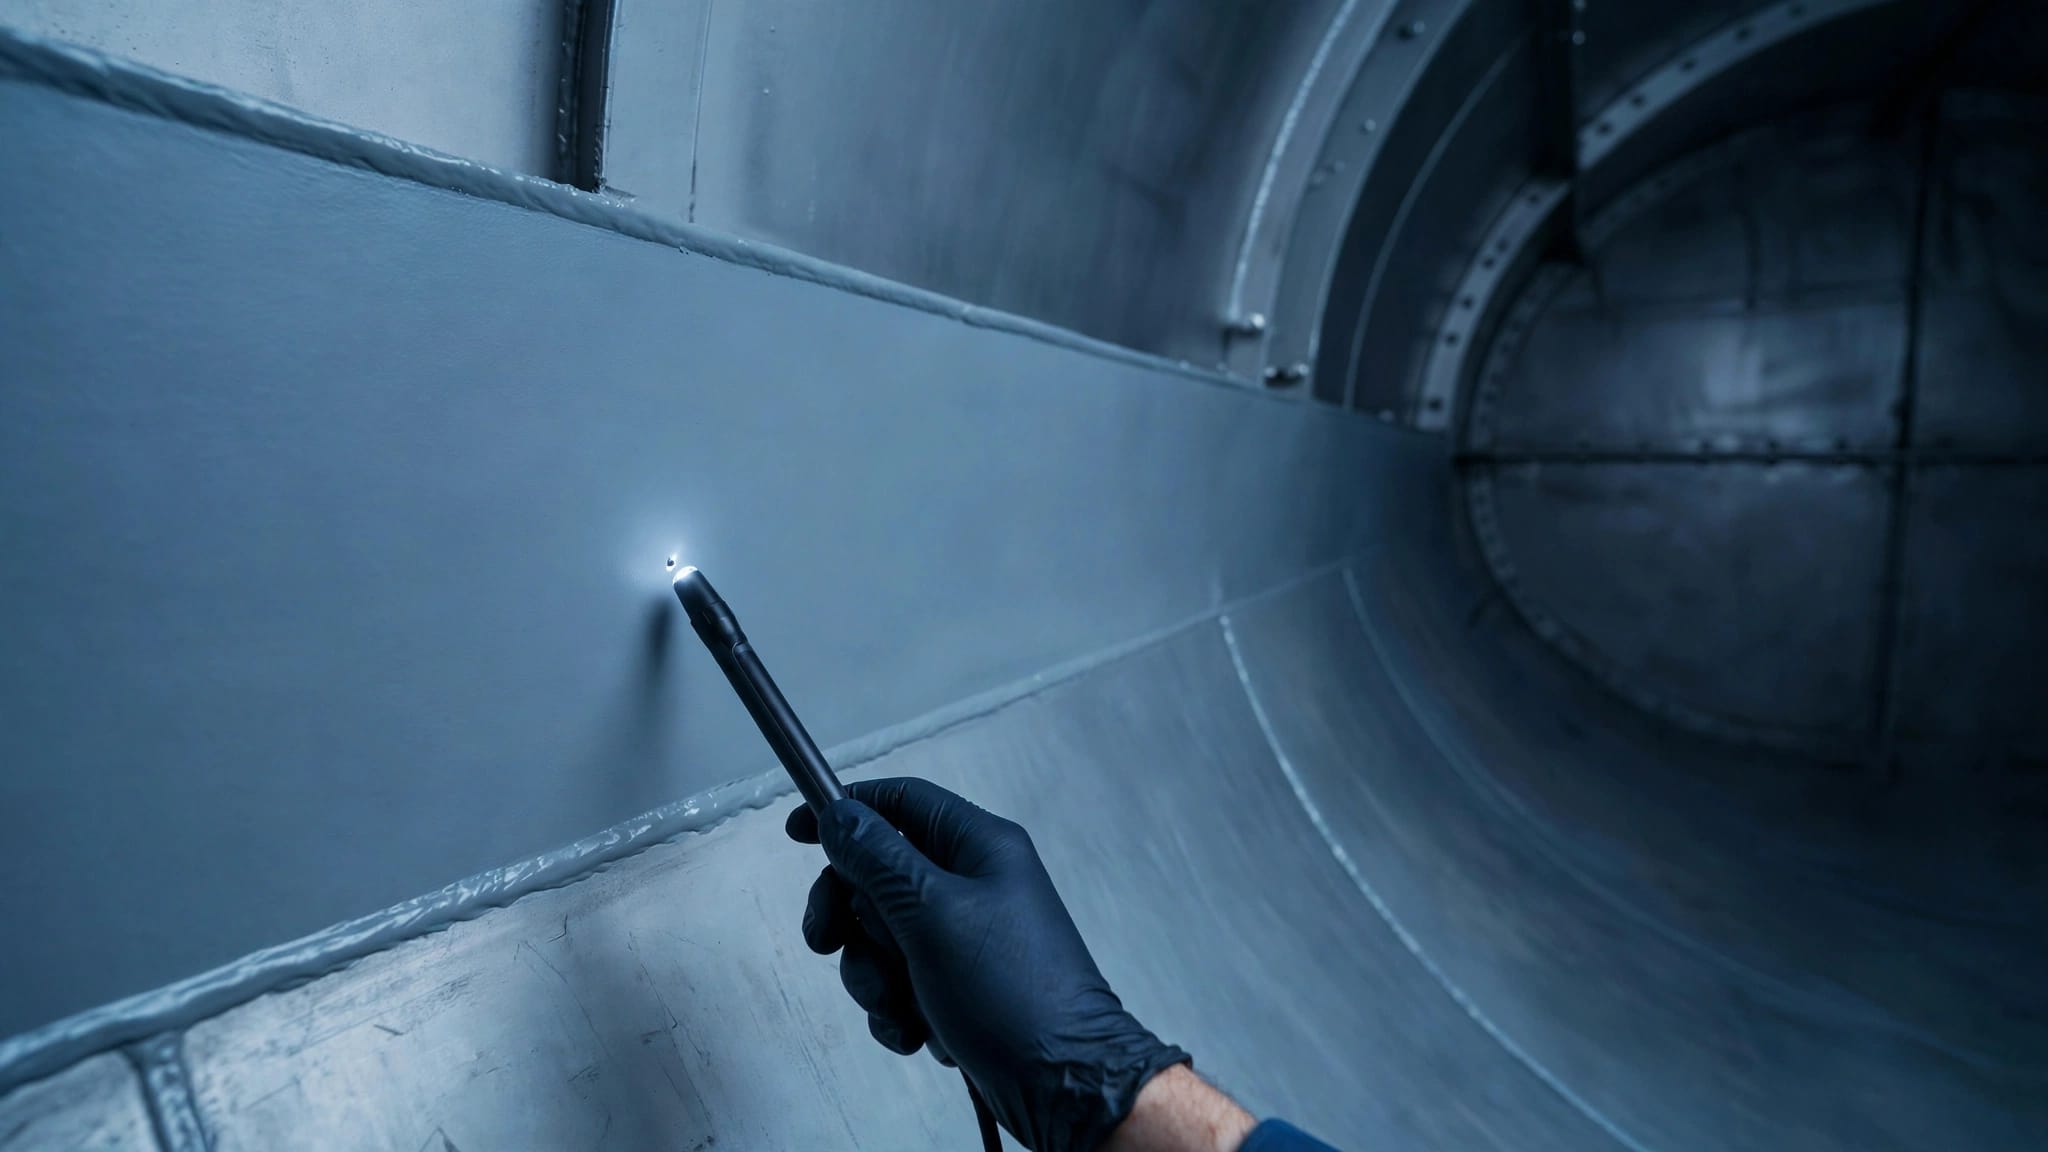
Visual inspection should include edges, corners, welds, fasteners, and other identified details. Inspectors look for missed areas, runs, sags, pinholes, and damage as well as general appearance.
Wet-film measurements help control application before the coating dries. However, they don't replace the specified final dry-film inspection.
Dry-film measurements also need an appropriate procedure and equipment. Tight geometry can complicate measurement, so readings on nearby flat steel shouldn't automatically stand in for the detail itself.
Excessive buildup deserves attention alongside inadequate coverage because some products develop curing or performance problems when applied outside their limits.
Keep inspection findings tied to project requirements
Different inspection methods answer different questions. Thickness measurements assess film build, while specified discontinuity testing identifies openings through an applicable coating or lining. Neither method establishes every aspect of coating performance.
The project should define inspection stages, methods, and acceptance criteria before work starts. Records should connect the findings to identifiable locations rather than describe the entire structure as simply "passed."
Our industrial coating inspection checklist helps organize condition observations and maintenance records. For completed work, useful documentation also includes product information, environmental readings, application dates, measured results, repair locations, and final findings.
Key Takeaways
- Stripe coating provides localized attention to difficult steel details while full coats cover the designated surface.
- Edges, welds, corners, and fasteners commonly deserve consideration, but the specification determines their treatment.
- Additional coating cannot replace contamination removal, fabrication correction, or structural repair.
- A complete proposal includes preparation, compatible products, application controls, and inspection requirements.
- Uniform color alone doesn't establish adequate coverage around complex geometry.
Frequently Asked Questions
Is stripe coating the same as touching up damage?
The two activities can address different needs. Stripe coating generally targets detail coverage within a planned coating process. Touch-up addresses localized damage, missed areas, or defects identified during application, handling, or service.
A damaged bolt head or weld may need a repair procedure that includes preparation and compatible coating. Simply labeling that work "striping" doesn't define the necessary repair. The scope should distinguish planned detail treatment from corrective work so the owner understands what the contractor has included.
Can additional coating seal an open joint?
An extra coating application shouldn't be treated as a substitute for a designed joint detail. Gaps, movement, trapped moisture, and inaccessible contact surfaces can require a separate approach.
Where a project needs sealant, repair material, or another joint treatment, that material must suit the coating system and service conditions. Bridging a gap with paint can leave concealed areas unprotected and may fail when the connection moves. The joint's condition needs attention before the finish covers it.
Protect the Details Within a Complete Coating Plan
Stripe coating can strengthen coverage at vulnerable steel details when the specified system calls for it. Its effectiveness still depends on sound preparation , compatible materials, and controlled application.
For your project, the useful starting point is a written scope identifying the steel's condition and exposure. The finished work should protect the connections and corners as deliberately as the open surfaces, with inspection records that document the result.
More featured articles...